

Industry news
By: Jetvision
Oct 29,2026
Metal injection molding (MIM) and conventional press-and-sinter powder metallurgy (PM) are both used to manufacture metal components from powder. However, they differ significantly in design flexibility, achievable properties, production costs and suitable applications.
Conventional powder metallurgy is often a cost-effective solution for relatively simple components that can be compacted and ejected along a defined pressing direction. MIM is particularly suitable for small, intricate metal parts that require complex three-dimensional geometry, good dimensional consistency and limited secondary machining.
Understanding these differences helps engineers and purchasing teams select the right manufacturing process before finalizing a component design.
Choose MIM for Complex Part Geometry
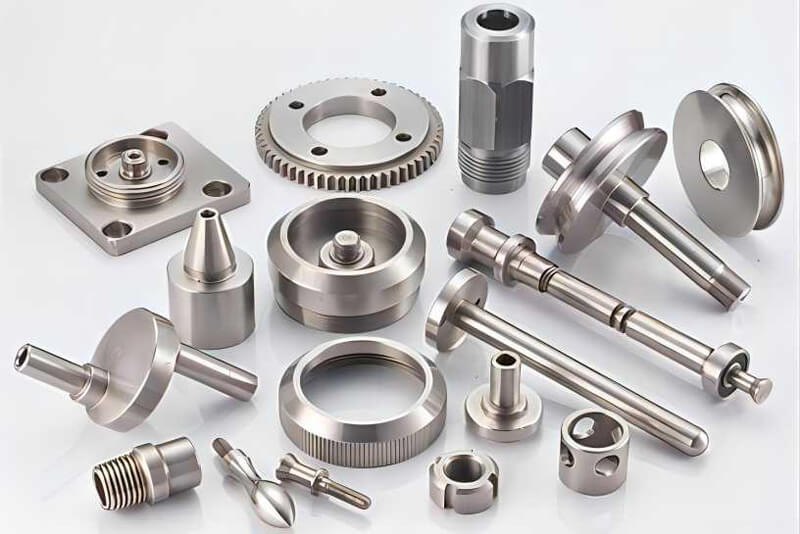
Part geometry is one of the most important factors when comparing MIM with conventional powder metallurgy.
Press-and-sinter PM uses rigid tooling to compact metal powder under pressure. Features that prevent straightforward die movement or interfere with part ejection may require additional tooling or machining.
MIM uses metal powder mixed with a polymer binder. The feedstock is injected into a mold, allowing more complex three-dimensional shapes to be produced.
MIM is worth considering for components featuring:
· Intricate three-dimensional shapes and stepped profiles
· Thin walls, small ribs and fine details
· Multiple functional features integrated into one component
· Complex external contours and miniature teeth
· Geometries that would otherwise require extensive CNC machining
MIM still has design limitations. Undercuts, internal passages and threads may require specialized tooling, side actions or secondary machining. Early design-for-manufacturing evaluation is essential to determine whether the required features can be molded economically.
Choose MIM When Mechanical Performance Is Critical
Conventional press-and-sinter PM can retain interconnected porosity, depending on the material and processing conditions. This is beneficial for applications such as oil-impregnated bearings but may limit mechanical performance in structural components.
MIM typically achieves a higher density than conventional pressed-and-sintered PM, which can support improved tensile strength, ductility and fatigue performance when the appropriate material and processing conditions are used.
MIM may be suitable for:
· Precision mechanical components subjected to repeated loading
· Small transmission and locking components
· Medical instrument parts
· Electronic and industrial hardware
· Components requiring good strength-to-size ratios
The actual mechanical properties depend on alloy composition, powder characteristics, debinding, sintering and any subsequent heat treatment. Engineers should compare certified material data and component-level test requirements rather than assuming that every MIM part will match wrought or forged materials.
Choose MIM for Small, Detailed Components with Tight Tolerances
MIM offers considerable design flexibility for small components with detailed surfaces and multiple dimensional requirements.
During sintering, MIM parts undergo substantial and predictable shrinkage that must be accounted for in mold design. Process control is therefore essential to maintain dimensional consistency across production batches.
For components with complex geometry, MIM can reduce the need for extensive milling, drilling or other machining operations. However, critical dimensions may still require secondary machining, sizing or finishing.
MIM is worth evaluating for miniature actuators, precision locking mechanisms, electronic hardware and other components where dimensional consistency and surface quality are important.
The appropriate process should be selected according to the drawing, tolerance requirements, material specifications and inspection criteria.
Choose MIM When It Reduces Total Manufacturing Cost
Conventional powder metallurgy often has a cost advantage for simple components that can be pressed efficiently with relatively straightforward tooling.
However, a low initial part price does not always mean a lower total manufacturing cost. If a PM component requires extensive machining, deburring, assembly or additional inspection, these operations can increase its final cost.
MIM may become more economical when it can:
· Consolidate multiple components into one part
· Reduce machining and assembly requirements
· Produce complex features directly during molding
· Support consistent, repeatable production at sufficient volumes
MIM generally involves more complex tooling and additional process stages, including debinding and sintering. Its economic advantage depends on part complexity, production volume, material selection, tooling investment and the amount of secondary processing avoided.
A detailed cost comparison should consider tooling, material consumption, cycle time, finishing, inspection, scrap and assembly rather than unit price alone.
When Conventional Powder Metallurgy Is the Better Choice
MIM is not always the most suitable option. Conventional press-and-sinter PM may be preferable when:
· The component has a simple shape that can be compacted and ejected easily.
· High production volumes favor a well-established pressing process.
· Controlled porosity is required, as in self-lubricating bearings.
· The component is relatively large or heavy for economical MIM production.
· The design does not justify the additional tooling and processing costs of MIM.
For these applications, conventional PM can provide a practical balance of production efficiency, material utilization and manufacturing cost.
How to Select Between MIM and Conventional PM
Before choosing a manufacturing process, evaluate the component's geometry, material, mechanical requirements and expected production volume.
Selection Factor | MIM | Conventional PM |
Part geometry | Complex, detailed 3D shapes | Relatively simple, pressable shapes |
Density | Generally higher | Depends on material and compaction process |
Mechanical properties | Often advantageous for dense, intricate parts | Suitable for many structural and porous applications |
Tooling and processing | More complex process and tooling | Often simpler for suitable geometries |
Secondary machining | May be reduced for complex parts | May be needed for features that cannot be pressed |
Typical cost advantage | Complex parts at sufficient production volumes | Simple parts with efficient pressing cycles |
These comparisons are general guidelines. Actual suitability should be confirmed through component design review, material evaluation and cost analysis.
The choice between metal injection molding and conventional powder metallurgy depends on the requirements of the finished component, not simply on the manufacturing technology.
MIM is often the stronger candidate for small, complex metal parts that combine intricate geometry, demanding dimensional requirements and a need to reduce secondary operations. Conventional PM remains highly competitive for simpler components, especially when controlled porosity or economical high-volume pressing is important.
At Jetvision, we provide MIM and powder metallurgy manufacturing solutions for different industrial component requirements. Our team can evaluate part drawings, material specifications, dimensional tolerances and production quantities to help determine a suitable manufacturing route.
Contact us to discuss your custom metal components and manufacturing requirements.
Back to Top