

Industry news
By: Jetvision
Nov 06,2026
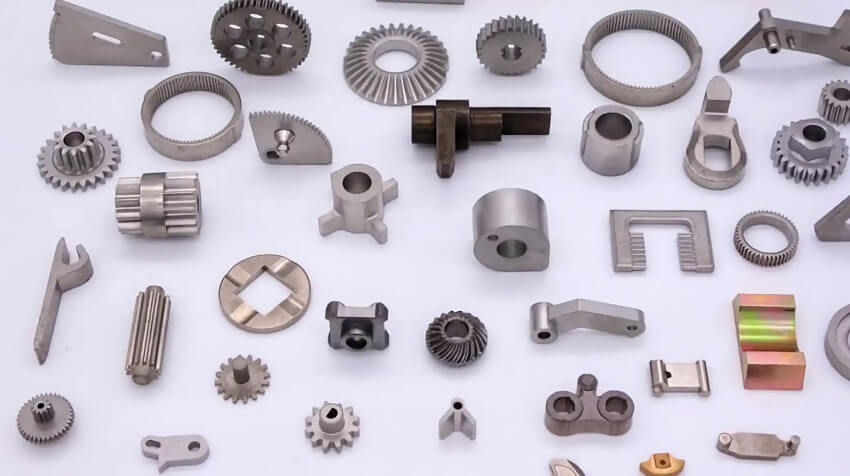
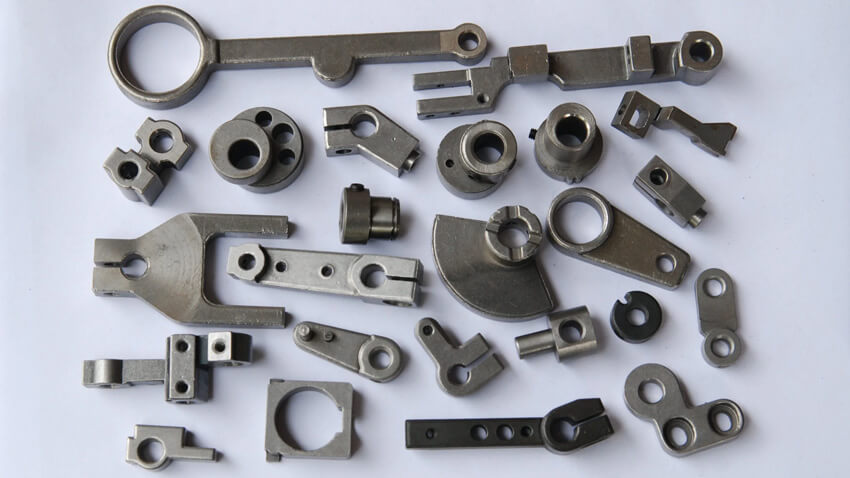
Custom powder metallurgy parts are often selected for components that require repeatable dimensions, complex geometries, efficient material utilization, and economical production at medium to high volumes. Applications range from automotive transmission systems and industrial gear assemblies to power tools, electrical equipment, and general machinery.
However, developing a successful powder metallurgy component involves more than converting a conventional machined part into a pressed metal powder product. The manufacturing process introduces specific engineering considerations related to powder flow, compaction direction, density distribution, sintering shrinkage, dimensional variation, and tooling limitations.
A component that performs well in a CAD model may not necessarily be suitable for conventional press-and-sinter manufacturing. Similarly, a prototype that meets dimensional requirements does not automatically guarantee stable performance during mass production.
For OEMs and engineering teams, the key is to establish a manufacturing strategy that connects component functionality with material characteristics, process capabilities, and production economics from the beginning of product development.
This article examines the major engineering considerations involved in developing custom powder metallurgy parts, from initial design evaluation to stable mass production.
Design for Manufacturing: Why PM Components Require a Different Design Approach
Design for Manufacturing (DFM) is one of the most important stages in custom powder metallurgy development.
Conventional machining starts with solid material and removes unwanted sections to achieve the required geometry. Powder metallurgy follows a different approach: metal powder is filled into a die cavity, compacted under pressure, and subsequently sintered.
This difference significantly influences component geometry.
Compaction Direction and Part Geometry
Conventional PM compaction generally applies pressure along a primary axis. As a result, component features must be evaluated in relation to the pressing direction.
Features such as vertical walls, stepped profiles, holes parallel to the pressing direction, and relatively uniform sections are generally easier to manufacture.
In contrast, transverse holes, undercuts, complex side features, and abrupt changes in section thickness may require additional tooling mechanisms or secondary machining.
For example, a gear hub with an axial bore and stepped outer profile may be suitable for conventional PM production, while a component with multiple radial holes may require additional processing after sintering.
Wall Thickness and Section Transitions
Large differences in wall thickness can create uneven powder filling and variations in compaction density.
These variations may contribute to differences in shrinkage, distortion, and mechanical properties during sintering.
Where possible, designers should avoid unnecessary abrupt transitions between thick and thin sections. Gradual transitions and appropriately designed radii can improve manufacturability and reduce stress concentrations.
Draft Angles and Ejection Considerations
Components must be released from the die after compaction without damaging the green compact.
Depending on the tooling configuration, draft angles and suitable surface geometry may improve ejection reliability. Features that create excessive friction or mechanical interference should be carefully evaluated during the design stage.
The objective is not simply to make a part geometrically producible, but to ensure that it can be compacted and ejected repeatedly without introducing defects.
Material Selection: Balancing Density, Strength, and Functional Requirements
Material selection for custom PM components should begin with the actual operating conditions rather than the nominal material designation.
Different applications impose different demands, including tensile loading, impact, wear, fatigue, corrosion, and dimensional stability.
Iron Based Powder Materials
Iron-based materials are widely used in conventional powder metallurgy because of their versatility and cost-effectiveness.
Depending on the powder system and subsequent processing, iron-based PM materials can be developed for structural components such as gears, sprockets, hubs, bushings, and mechanical supports.
Copper Based Materials
Copper-based powder metallurgy materials are suitable for applications requiring electrical or thermal conductivity, as well as selected friction-related functions.
Their suitability depends on the required conductivity, density, geometry, and operating environment.
Stainless Steel Powder Materials
Stainless steel PM materials are considered when corrosion resistance is a primary requirement.
Applications may include industrial equipment components, fluid-handling assemblies, and parts exposed to humid or chemically aggressive environments.
Alloyed Powder Materials
Pre-alloyed and diffusion alloyed powders containing nickel, copper, molybdenum, and other alloying elements can be used to achieve different combinations of strength, hardenability, and wear resistance.
The final properties depend not only on the powder composition but also on green density, sintering conditions, cooling characteristics, and any subsequent heat treatment.
An important engineering consideration: Material selection and component design should be evaluated together. A material that meets the required strength level may still be unsuitable if its compressibility, sintering behavior, or dimensional response makes the intended component difficult to manufacture consistently.
Density Distribution: A Critical Factor in PM Component Performance
Density is one of the most important parameters affecting the performance of conventional powder metallurgy parts.
Unlike fully dense wrought or machined components, sintered PM parts typically contain a controlled amount of porosity. Their density is therefore closely related to the selected powder system and manufacturing conditions.
However, average density alone does not provide a complete picture of component quality.
Why Density Uniformity Matters
During compaction, powder particles rearrange and deform under applied pressure. If powder filling or pressure transmission is uneven, different regions of the component may develop different green densities.
These variations can influence:
· Local shrinkage during sintering
· Dimensional consistency
· Tensile and fatigue properties
· Hardness distribution
· Resistance to impact and mechanical loading
For components exposed to cyclic loading or high mechanical stress, density distribution deserves particular attention.
Balancing Density and Manufacturing Feasibility
Increasing compaction pressure can help achieve higher green density, but it is not a universal solution.
The appropriate pressure depends on powder compressibility, material characteristics, tooling strength, and component geometry.
Excessive or poorly controlled compaction conditions can increase tooling loads and contribute to defects such as lamination or cracking.
For this reason, density requirements should be established according to the component's actual mechanical and functional demands.
A suitable PM manufacturing process aims to achieve the required density and uniformity without introducing unnecessary production complexity or cost.
Tooling Design and Dimensional Compensation
Tooling design has a direct influence on dimensional accuracy, production efficiency, and the long term economics of custom powder metallurgy parts.
Unlike many machining operations, PM production relies on dedicated dies and punches to form the component geometry. Tooling must therefore account for both the initial compacting operation and subsequent dimensional changes.
Understanding Sintering Dimensional Changes
During sintering, metal particles bond through diffusion mechanisms. Depending on the material system, green density, and sintering conditions, the component may undergo shrinkage, expansion, or relatively small dimensional changes.
This behavior must be considered when designing the die cavity.
Dimensional compensation is not simply a matter of applying a universal shrinkage percentage. It should be established through material-specific process knowledge and verified through trial production.
Tooling Accuracy and Wear
Tooling dimensions can gradually change through repeated production cycles.
Wear on die surfaces and punches may affect critical dimensions, particularly for components with tight tolerances or high production volumes.
A practical tooling strategy should consider:
· Critical dimensional requirements
· Die and punch material selection
· Expected production quantities
· Tool wear monitoring
· Maintenance and replacement intervals
· Feasibility of dimensional correction through secondary operations
Good tooling design helps maintain consistency throughout the production lifecycle rather than focusing only on the first approved sample.
Compaction and Sintering: Establishing a Stable Manufacturing Window
Compaction and sintering are closely connected processes. Their parameters should be developed as part of an integrated manufacturing strategy.
Powder Filling and Compaction Control
Consistent powder filling is essential for achieving repeatable green compact dimensions and density.
Factors such as powder particle size distribution, apparent density, flow characteristics, lubricant content, and filling behavior can affect the compaction process.
For components with complex profiles, powder distribution inside the die becomes particularly important.
During production development, manufacturers should evaluate filling consistency, pressing conditions, green strength, and ejection behavior.
Sintering Atmosphere and Temperature Control
Sintering temperature alone does not determine the final properties of a PM component.
The furnace atmosphere, heating rate, holding time, cooling rate, and material composition all influence the metallurgical bonding process.
For iron-based materials, the atmosphere and carbon potential may also influence oxidation and carbon balance.
Poorly controlled sintering conditions can result in insufficient particle bonding, dimensional variation, oxidation, or inconsistent mechanical properties.
The objective is to establish a stable process window that delivers repeatable results across production batches.
Secondary Processing: When Press and Sinter Is Not Enough
One advantage of conventional powder metallurgy is its ability to produce near-net-shape components. However, not every functional requirement can be achieved directly through compaction and sintering.
Secondary operations should be selected according to the component's critical dimensions, mechanical properties, and operating environment.
Secondary process | Main purpose |
Sizing | Improve dimensional accuracy and consistency |
Coining | Refine specific surfaces and geometrical features |
Machining | Produce precision holes, threads, bores, and critical profiles |
Heat treatment | Improve hardness, strength, and wear resistance |
Steam treatment | Improve surface characteristics and selected corrosion or wear properties |
Impregnation | Fill interconnected pores with oil or resin for specific functional requirements |
Plating | Provide suitable surface protection or functional characteristics |
An important consideration is that secondary machining may expose internal porosity. This can affect sealing, surface appearance, and functional performance.
For components requiring pressure tightness, fluid containment, or specific surface integrity, these factors should be evaluated before finalizing the design.
A well-planned process should minimize unnecessary secondary operations while ensuring that all functional requirements are achieved.
Quality Control: Connecting Process Parameters with Final Component Performance
For custom PM parts, final inspection alone is insufficient to guarantee stable production quality.
Quality control should cover the entire manufacturing process, with inspection criteria linked to the component drawing and its intended application.
Dimensional Verification
Critical dimensions should be identified during engineering review.
Depending on the component geometry, inspection may include outer diameter, inner diameter, height, thickness, concentricity, flatness, and positional accuracy.
It is also important to distinguish between dimensions that can be controlled through tooling and those that require secondary machining.
Density and Mechanical Testing
Density measurement provides important information about the compacted and sintered structure.
Where required, hardness, tensile strength, transverse rupture strength, and other mechanical properties can be evaluated according to the applicable material and product specifications.
Microstructure and Porosity Evaluation
Metallographic examination can help assess pore distribution, particle bonding, and microstructural characteristics.
For components with demanding mechanical requirements, this information can provide additional insight beyond conventional dimensional inspection.
Production Consistency
For mass production, inspection should also monitor process variation between batches.
A component that meets specifications in one production run should continue to meet the agreed requirements during subsequent manufacturing cycles.
Establishing clear acceptance criteria and traceable inspection records helps support this consistency.
Scaling from Prototype to Mass Production: The Importance of Process Validation
The transition from prototype development to mass production is often where the most important manufacturing challenges emerge.
Initial samples are generally produced in relatively small quantities. Once production volume increases, tooling wear, powder consistency, furnace loading, process variation, and production efficiency become more significant.
A successful development program should therefore include more than sample approval.
1. Engineering Review
Review drawings, functional requirements, material specifications, tolerances, and annual demand.
Identify features that may affect compaction, ejection, sintering, and secondary processing.
2. Tooling and Initial Samples
Develop production tooling and manufacture trial components.
Evaluate green compact integrity, sintering behavior, dimensions, density, and required mechanical properties.
3. Process Optimization
Adjust tooling compensation, powder filling, compaction conditions, sintering parameters, and secondary operations.
The objective is to achieve a repeatable process rather than simply producing one acceptable sample.
4. Production Validation
Run a representative production batch to evaluate process stability, tooling performance, inspection consistency, and production capacity.
5. Continuous Production Control
Once the process is approved, maintain established production parameters and monitor critical quality characteristics throughout subsequent batches.
For OEM customers, this development approach reduces the risk of unexpected dimensional or performance variation after production volumes increase.
Evaluating the Economics of Custom Powder Metallurgy Manufacturing
The economic advantage of powder metallurgy depends on the relationship between tooling investment, component complexity, material utilization, secondary processing, and production volume.
Although dedicated tooling requires an initial investment, the cost per component can decrease significantly when production quantities are sufficient.
However, the lowest initial tooling cost does not necessarily result in the lowest total manufacturing cost.
A comprehensive cost evaluation should consider:
· Initial tooling and development costs
· Powder material costs and utilization
· Compaction and sintering cycle efficiency
· Secondary machining requirements
· Inspection and quality assurance
· Tooling maintenance and service life
· Annual production demand
For relatively simple components with high annual demand, conventional PM can offer substantial cost advantages.
For low volume components with extensive machining requirements or complex geometries, alternative manufacturing methods may be more economical.
The most appropriate manufacturing route should therefore be determined through a combination of technical feasibility and total production cost analysis.
Building Reliable Custom PM Components Through Engineering and Process Control
Developing custom powder metallurgy parts from design to mass production requires an integrated understanding of component geometry, powder characteristics, material behavior, compaction, sintering, tooling, and quality control.
The most successful PM projects are not simply those that achieve the required dimensions in initial samples. They are those that establish a stable and economical manufacturing process capable of delivering consistent quality over repeated production cycles.
At Jetvision, custom powder metallurgy manufacturing projects are evaluated according to customer drawings, material requirements, dimensional specifications, and application conditions. From initial design assessment and tooling development to sample verification and batch production, the focus is on manufacturing feasibility, process consistency, and dependable OEM component supply.
Have a custom PM component drawing or an upcoming production project? Contact Jetvision to discuss material selection, manufacturing feasibility, tooling requirements, and mass production solutions.
Back to Top